en
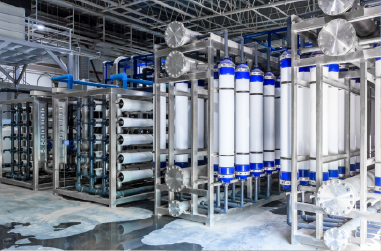
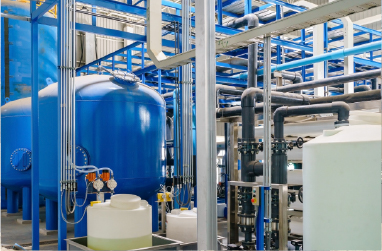
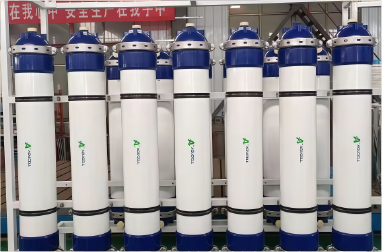
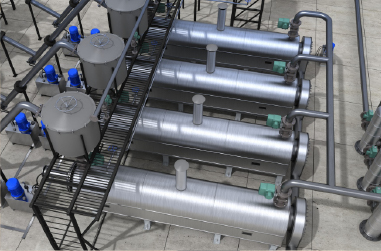
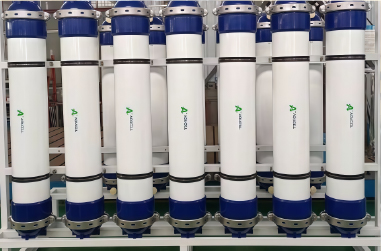
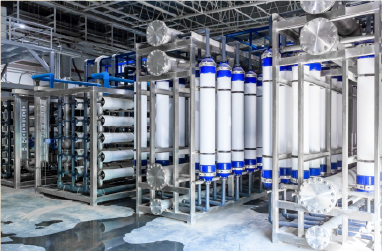
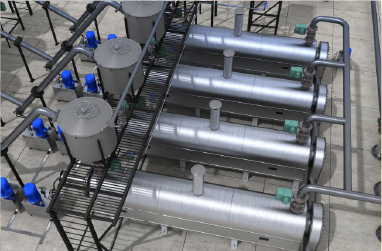
Membrane concentration equipment is a highly efficient concentration system based on membrane separation technology. It selectively separates solvents and solutes in materials through semi-permeable membranes, achieving rapid material concentration. Widely applied in food, pharmaceuticals, chemicals, environmental protection, and other industries.
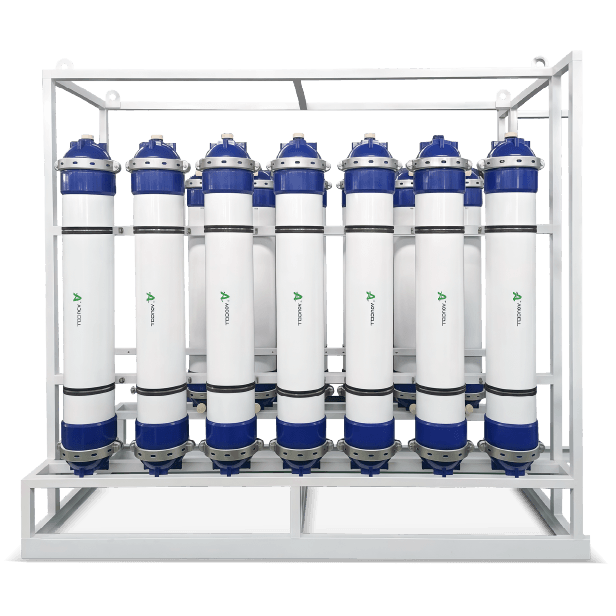
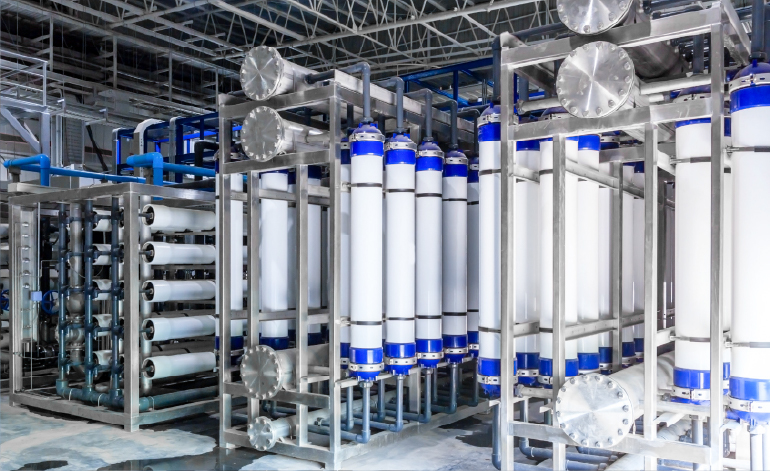
Leveraging the selective permeability of membranes, it achieves material concentration at room temperature, preventing thermal damage to heat-sensitive components while preserving original flavors and active ingredients. Concentration efficiency is over 30% higher than traditional evaporation equipment.
Requires no heating or only minimal low-temperature assistance, consuming merely 1/3 to 1/5 of the energy used by conventional evaporation systems, significantly reducing production energy costs.
Equipped with an intelligent control system for real-time monitoring of pressure, flow rate, concentration, and other parameters during the process, enabling automated operation with minimal manual intervention.
Tailored membrane materials (e.g., ultrafiltration, nanofiltration, reverse osmosis) and equipment specifications can be designed based on material properties (viscosity, composition, concentration) and production needs, suitable for scenarios ranging from lab-scale trials to industrial-scale production.

Using membrane selective permeability, it concentrates materials at room temperature, avoiding heat damage to sensitive components and preserving flavors and actives. Its efficiency is over 30% higher than traditional evaporation. 询问 ChatGPT

Requires no heating or only minimal low-temperature assistance, consuming merely 1/3 to 1/5 of the energy used by conventional evaporation systems, significantly reducing production energy costs.

Equipped with an intelligent control system for real-time monitoring of pressure, flow rate, concentration, and other parameters during the process, enabling automated operation with minimal manual intervention.

Tailored membrane materials (ultrafiltration, nanofiltration, reverse osmosis) and equipment are designed based on material properties and production needs, suitable for lab trials to industrial-scale production.
Ideo urbs venerabilis post superbas effer atarum gentium cervices oppressas latasque leges fundamenta libertatis et retinacula
Ideo urbs venerabilis post superbas effer atarum gentium cervices oppressas latasque leges fundamenta libertatis et retinacula

Quanta autem vis amicitiae sit, ex hoc intellegi maxime potest, quod ex infinita.

Haec ubi latius fama vulgasset missaeque relationes adsiduae Gallum Caesarem.

Haec ubi latius fama vulgasset missaeque relationes adsiduae Gallum Caesarem.

Haec ubi latius fama vulgasset missaeque relationes adsiduae Gallum Caesarem.
Ion exchange resins are a type of polymeric spherical particles with functional groups that achieve the separation, purification, and purification of ions in water or materials through ion exchange reactions. They are widely used in water treatment, pharmaceuticals, chemicals, food, and other industries, serving as efficient separation and purification materials.
Membrane concentration equipment is a highly efficient concentration system based on membrane separation technology. It selectively separates solvents and solutes in materials through semi-permeable membranes, achieving rapid material concentration. Widely applied in food, pharmaceuticals, chemicals, environmental protection, and other industries.
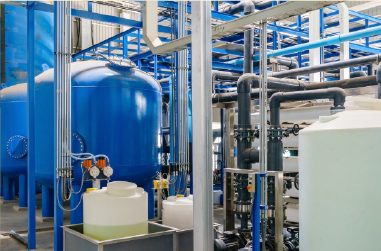
Ion exchange system is a high-efficiency separation and purification equipment based on ion exchange resin technology. It utilizes the ion exchange reaction between resin and ions in water or materials to achieve impurity removal and substance purification. Widely applied in water treatment, pharmaceuticals, chemicals, food, dyeing, and other industries.
Our gelatin production line is a fully automated system specifically designed for gelatin manufacturing, covering the entire process from raw material processing, extraction, purification, concentration, to drying. It meets the production needs of various scales and is widely applied in food, pharmaceuticals, chemicals, and other industries.
Quaestione igitur per multiplices dilatata fortunas cum ambigerentur quaedam, non nulla levius actitata constaret, post multorum clades Apollinares ambo pater et filius.
Quaestione igitur per multiplices dilatata fortunas cum ambigerentur quaedam, non nulla levius actitata constaret, post multorum clades Apollinares ambo pater et filius.


